


Polyvinyl Alcohol Market Innovations Transforming Next-Generation Packaging, Coatings, Adhesives, and Specialty Polymer Applications
Growing interest in innovative packaging materials is encouraging manufacturers to explore polymers that combine film-forming ability, flexibility, and specialized barrier properties. Polyvinyl alcohol (PVA) is gaining attention because it can form clear, uniform films and can be processed into water-soluble packaging formats. Its properties make it useful in applications where controlled dissolution, product protection, and efficient packaging design are important. Manufacturers are incorporating PVA into specialized films for household products, industrial chemicals, and selected packaging applications.
The Polyvinyl alcohol Market is benefiting from demand for water-soluble films used in unit-dose packaging, including detergent pods and other premeasured products. These films can dissolve under specified conditions, allowing consumers to use packaged products without directly handling concentrated formulations. PVA's film-forming characteristics and adjustable solubility make it suitable for developing packaging grades with different thicknesses and dissolution profiles. Product developers select polymer grades according to the required strength, processing conditions, and intended use.
The growth of household cleaning products is an important factor supporting this application. Single-dose laundry and dishwasher products rely on packaging that can contain concentrated liquids or powders while remaining convenient to handle. PVA films help manufacturers create individual portions with controlled dimensions and sealing characteristics. Consistent film quality is essential because packaging must maintain its integrity during storage, transport, and handling before dissolving during use.
PVA is also being evaluated in specialty packaging and multilayer film structures. Its oxygen barrier properties under suitable conditions can contribute to packaging designs intended to protect sensitive products. However, its performance is influenced by humidity because moisture absorption can affect mechanical strength and barrier characteristics. Manufacturers therefore consider storage conditions, film thickness, blending materials, and protective layers when designing PVA-based packaging.
Technological progress is improving film production through advances in extrusion, casting, drying, and quality control. Formulators are also exploring blends with starch, cellulose derivatives, and other polymers to adjust flexibility, strength, and environmental performance. These combinations can help address application-specific requirements, although compatibility and processing behavior must be carefully evaluated.
Challenges include moisture sensitivity, raw material costs, and the need to establish suitable end-of-life conditions. Water solubility does not automatically mean that every PVA product will biodegrade rapidly in all environments. Its environmental performance depends on formulation, wastewater treatment, and disposal conditions. Clear product design and appropriate infrastructure are therefore important considerations.
Looking ahead, demand for convenient unit-dose packaging and specialty films is expected to create opportunities for PVA manufacturers. Suppliers that develop reliable, application-specific grades and efficient film-processing technologies may strengthen their position as packaging companies seek new functional materials.
Категории
Больше
Finding the best WiFi connection in Bangalore near me has become important for households, professionals, students, and businesses that depend on a stable internet connection every day. From work-from-home meetings and online classes to entertainment, gaming, cloud applications, and video calls, a dependable WiFi connection helps users stay connected without unnecessary interruptions. Bangalore...
Retail Mobile Phone Chargers Market size was valued at USD 6.29 billion in 2025. The market is projected to grow from USD 6.58 billion in 2026 to USD 9.87 billion by 2034, exhibiting a CAGR of 4.7% during the forecast period. Download Sample Report Market Insights Global Retail Mobile Phone Chargers Market size was valued at USD 6.29 billion in 2025. The market is projected to grow from USD...

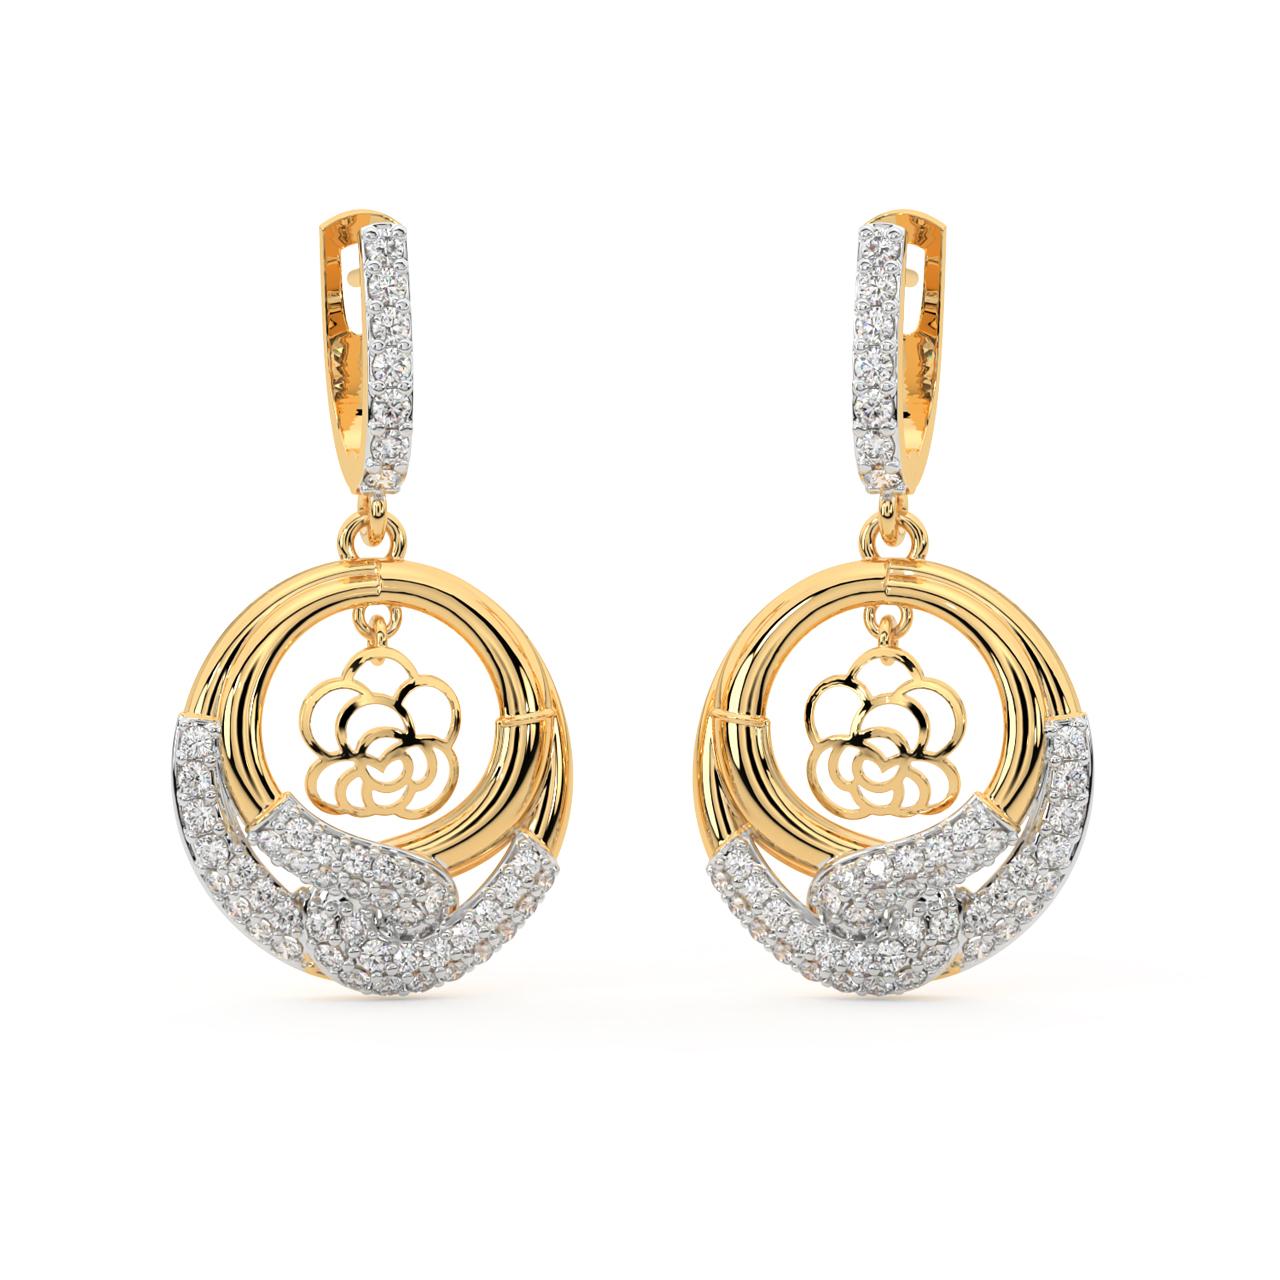
Gold Earrings Designs for Daily Use – Elegant & Comfortable Choices for Everyday Style Gold earrings are one of the most essential pieces of jewelry in every woman’s collection. When it comes to gold earrings designs for daily use, the focus is always on comfort, simplicity, and timeless beauty. Whether you are heading to the office, college, or just stepping out casually, the...
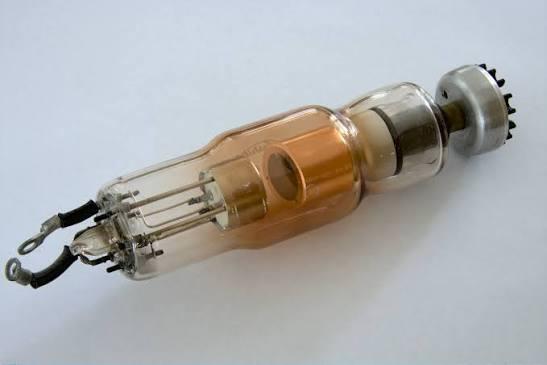
Establishing precise empirical models of diagnostic component distribution requires robust research methodologies that track raw material supply chains, component manufacturing output, and global scanner installation bases. Researchers analyzing the diagnostic equipment ecosystem utilize multi-tier data integration methods, combining tungsten and molybdenum metal shipment figures with...
Non metal electrical conduit manufacturers are moving beyond commodity production toward integrated systems that combine physical protection with digital capability, as construction and electrical contracting demand more than a rigid tube. According to Market Research Future, the non metal electrical conduit manufacturers landscape is moderately fragmented, with Schneider Electric, Legrand,...