CenWan Construction for Folder Gluer Machine Manufacturers Versatility
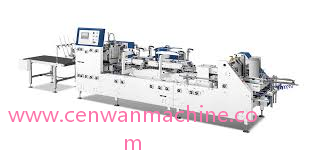
Packaging converters who run mixed product portfolios frequently evaluate the range of substrates that equipment can process without frequent adjustment or quality variation. Builders known as Folder Gluer Machine Manufacturers including cenwanmachine engineer feed systems folding belts and adhesive applicators that accommodate both solid paperboard and corrugated constructions across a practical thickness spectrum. The central inquiry concerns the capacity of these mechanical and control features to deliver uniform fold lines and bond strength once material properties change from job to job?
Paperboard grades used for folding cartons typically range from lightweight stock suited to small retail packs through heavier boards intended for larger display or pharmaceutical cartons. The feed section must separate individual blanks cleanly without double feeding or edge damage. Vacuum assisted belts and adjustable side guides maintain alignment while the board travels into the pre-break and folding stations. Consistent pressure across the blank width prevents skew that would otherwise produce uneven glue flaps.
Corrugated constructions introduce additional variables. Single wall B flute E flute and microflute boards present different crush resistance and surface friction. The machine must apply sufficient folding force to crease along the scored lines without crushing the flutes or distorting the overall blank geometry. Adjustable roller pressure and belt tension allow operators to match the compressive load to the specific flute profile so the finished box retains its intended dimensional stability.
Surface treatments further influence process behavior. Uncoated board accepts cold glue readily and develops bond strength under moderate compression. Coated or laminated surfaces often require hot melt adhesive whose viscosity and open time differ from standard PVA formulations. Nozzle temperature control and precise volumetric metering ensure the adhesive bead remains continuous and correctly placed even when the board surface energy varies. Sensor feedback can interrupt the glue cycle if blank position drifts outside tolerance.
Blank size variation places demands on the transport system. Narrow blanks for small cartons travel at higher linear speeds while wide blanks for large trays or shippers require stable support across the full width. Segmented belts and independent side guides maintain contact without excessive friction that could mark the printed surface. The folding section itself uses parallel belts whose gap can be adjusted to the final folded thickness so the box emerges square and ready for packing.
Adhesive transfer reliability depends on both the applicator and the subsequent compression section. The glue wheel or nozzle must deposit a consistent volume along the designated flap edge. Compression rollers or belts then hold the joint closed while the adhesive sets. For hot melt systems the compression distance is shorter because the bond forms rapidly. For cold glue longer compression paths provide the dwell time needed for full strength development. Modular compression units allow the line to switch between these modes with minimal mechanical changeover.
Operator interface and job memory functions support rapid adaptation when material type changes. Stored parameters for belt speeds roller pressures and glue volumes can be recalled for recurring substrates so setup time remains short. Visual confirmation of fold quality and bond appearance during the first few blanks allows fine adjustment before full production resumes. These features reduce the risk of waste when the next order introduces a different board grade or coating.
Production environments that handle both folding carton and corrugated work benefit from machines whose mechanical range covers the required spectrum without specialized tooling for each category. Shared components such as the feeder and main drive reduce inventory of spare parts while interchangeable folding sections address the distinct geometry of straight line crash lock or multi corner styles. The overall configuration therefore supports a mixed order book without dedicated lines for each substrate family.
Maintenance practices influence long term material handling consistency. Regular inspection of belt surfaces vacuum cups and glue nozzles prevents gradual degradation that could affect feed reliability or adhesive placement. Wear items are designed for straightforward replacement so downtime remains limited. Documentation accompanying the equipment lists recommended intervals and procedures matched to the expected mix of board types.
Converters who process a broad range of packaging styles often request demonstration runs with their own substrates. Test records document fold accuracy bond strength and residual scrap rates across the sample set. When these results accompany the machine specification the purchaser can confirm suitability for the intended product mix and production volume. In facilities where both lightweight cartons and heavier corrugated shippers share the same floor space the ability to process both categories on a single platform simplifies scheduling and reduces capital commitment.
At the final stage of each production cycle the finished boxes accumulate in a stacker or exit conveyor prepared for packing. Consistent material handling throughout the preceding stations ensures that the stacked product remains uniform in appearance and structural integrity. Clear labeling of machine capabilities regarding board weight range flute types and coating compatibility assists procurement teams in matching equipment to current and anticipated orders.
Packaging operations seeking reliable processing across varied substrates can examine configuration details of available systems at the address https://www.cenwanmachine.com/product where Folder Gluer Machine Manufacturers such as cenwanmachine present notes on feed systems folding geometry and adhesive modules that accommodate paperboard and corrugated grades under continuous operation. Matching equipment whose mechanical range accounts for differences in thickness surface and structure with the requirements of the product portfolio supports consistent output throughout mixed production schedules.
Categorías
Read More
Infrastructure development in the United States continues to expand as transportation networks, erosion control systems, and environmental protection projects receive increasing investment. Geotextiles have emerged as essential materials in civil engineering because they improve soil stabilization, drainage, filtration, and reinforcement performance. These permeable fabrics are widely used in...
The functional food landscape is being continuously enriched by ingredients that go beyond basic nutrition to deliver targeted health benefits, and dairy protein crisps are rapidly emerging as a transformative player in the realm of Functional Food Ingredients . As per Market Research Future, these versatile crisps are redefining how the industry approaches the intersection of...
Некоторые заявляют, будто бы пластмассу необходимо запретить. Ну а другие кричат, что надо еще больше вещей делать из пластмассы, а кроме того строить перерабатывающие заводы. Если объективно и честно посмотреть на данную картину, понятно станет: в общем-то ошиблись все. Например на текущий день отказаться от пластмассы нереально, так как придется забыть про окна, авто, смартфоны,...
In recent years, wellness-focused gatherings have become a major trend, with people looking for unique ways to celebrate, relax, and connect. One of the most exciting additions to this trend is sauna experiences brought directly to private or group events. Whether it is a corporate gathering, birthday celebration, retreat, or pre-wedding celebration, sauna experiences create a relaxing and...
Anti-VEGF therapies are the cornerstone of the choroidal neovascularization market. Drugs that inhibit vascular endothelial growth factor reduce abnormal blood vessel growth and leakage, preserving vision in patients with CNV. Since their introduction, these therapies have transformed treatment and expanded the market. In the choroidal neovascularization market, competition among anti-VEGF...